

Cellulose Acetate
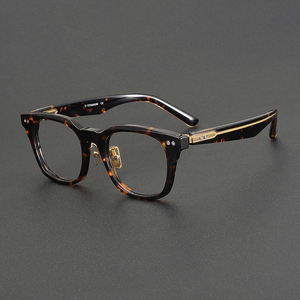
Engineered from premium cellulose acetate, carbon fiber composite, and vacuum IP-plated titanium. Designed for high-end optical labs, fashion brands, and private label distributors.
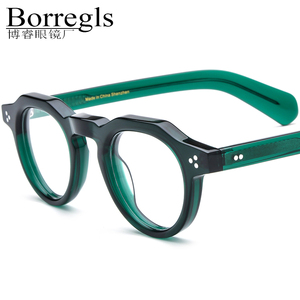
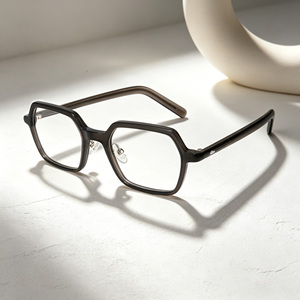
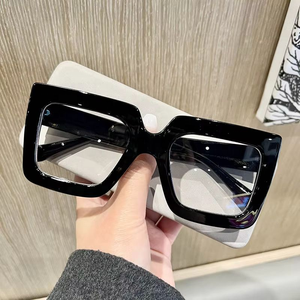
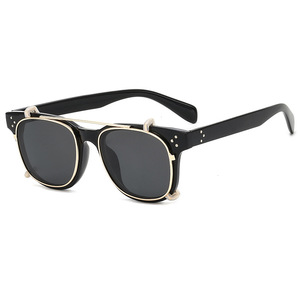
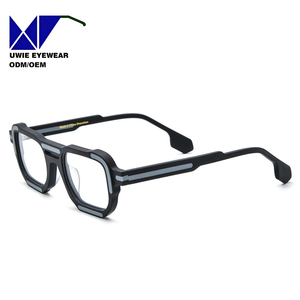
Geometric eyewear—encompassing octagonal, hexagonal, crown panto, and beveled architectural square silhouettes—has transitioned from niche high-fashion runways into volume optical retail. Sourcing managers must evaluate the engineering underlying modern architectural frames.
Conventional flat-face eyewear is being superseded by complex 3-dimensional profile milling. Using multi-axis CNC tooling, our facility executes precise compound facets along the brow-line and eyewire edges. This diamond-cut geometric architecture captures light dynamically while paring down total frame weight by up to 22% compared to standard monolithic acetate blanks.
In accordance with Global Recycled Standard (GRS) and ISO 14855 standards, modern retail demands non-petroleum based plasticizers. We manufacture geometric silhouettes utilizing renewable wood pulp and cotton lint cellulose acetate, replacing diethyl phthalate with organic triethyl citrate. This retains high plastic memory and heat-adjustability while reducing product carbon footprints.
The confluence of high-rigidity beta titanium with organic acetate sheet creates modern architectural strength. Our patented wire-core insertion and heat-compression laminate methodologies allow ultra-slim 2.8mm geometric rims that hold prescriptions up to -8.00 diopters without ocular rim distortion, cold-cracking, or lens slippage during optical bench glazing.
Unlike commercial injection-molded eyewear that distorts under thermal shifts, high-grade geometric frames require stringent laboratory testing. Our workshop integrates internal quality control protocols aligned with ISO 12870 and ANSI Z80.5 optical parameters.
Every production batch undergoes continuous stress analysis: bridge fatigue endurance tests, tumbling-cycle colorfastness, nickel-release spectrographic assays, and 72-hour salt-spray salt-fog resistance on all metal core assemblies.
Get a Quote| Testing Dimension | Global Industry Base | Factory Standard | Compliance Status |
|---|---|---|---|
| Rim Groove Tolerance | ±0.15 mm | ±0.05 mm | Lab Certified |
| Hinge Endurance Test | 5,000 Cycles | 20,000 Cycles | ISO 12870 Pass |
| Acetate Curing Period | 10 - 15 Days | 45 Days (Stable) | De-Stressed |
| Nickel Leaching Assays | <0.5 μg/cm²/wk | 0.00 μg (Nickel-Free) | REACH Certified |
| Surface Polish Depth | 2-Stage Barrel | 4-Stage + Wheel Buff | Mirror Gloss |
Bridging the gap between creative industrial sketches and scalable, defect-free volume shipments. Our systematic sample-first methodology guarantees consistency across production batches.
Translating styling sketches into precise technical 2D/3D CAD drawings. Optimizing boxing dimensions (lens, bridge, and temple clearance) for demographic ergonomics.
Curing premium organic acetate blocks in climate-controlled rooms to release internal stresses, followed by 5-axis CNC roughing and high-speed fine edge-chamfering.
Ultrasonic wire-core shooting into temples and precision CNC pocket routing for high-torque 3-barrel, 5-barrel, or German-engineered OBE spring hinges.
Up to 96 hours of progressive tumbling in walnut shells, birch chips, and pumice paste, concluded by artisan hand-buffing on cotton wheels for optical lustre.
Hot-wire lens mounting verification, permanent laser pad printing, drop-ball impact verification, and multi-tier boxing inside export-ready freight master cartons.
Operating since 1985 with over 40 years of continuous category leadership, we provide the supply chain transparency, engineering agility, and material fidelity required by discerning optical brands.
Founded in 1985, our specialized workshops have concentrated exclusively on structural optical frames, sunglasses, and custom lifestyle eyewear. This institutional craftsmanship is embedded in cutter geometries, sheet shrinkage compensation ratios, and finishing finesse.
Access a running inventory of over 22 proprietary master chassis platforms and 258 distinct colorways. Our rapid-adaptation ODM service allows commercial importers to modify eyewire dimensions, bridge spans, and temple styles without the upfront capital expense of new injection tooling.
We maintain absolute client confidentiality. From micro-laser logo etchings and pad printing to barcoded secondary luxury hard cases, lens protective films, and retail display outer boxes, no factory identifiers remain on outbound goods.
Detailed answers addressing minimum order volumes, material stability, surface treatment, and shipping compliance for technical optical buyers.
For custom geometric OEM production from existing master acetate tooling, our standard MOQ is typically 300 to 500 pairs per model, divided across 2–3 acetate colorways. Tailored physical prototypes for bench approval are fabricated within 14–20 business days. Bulk batch production cycles conclude within 45–60 days depending on raw material customization and curing requisites.
Angular silhouettes (such as hexagons, octagons, and crown pantos) carry localized stress points at outer corner junctions. We mitigate internal stress through a double-aging annealing cycle: acetate blanks are kiln-conditioned for 45 days at regulated humidity before CNC cutting, followed by a secondary low-temperature baking step prior to barrel polishing. This eliminates frame shrinkage and warping over extended storage periods.
Yes. Our CNC rim grooves are cut with specialized V-bevel cutters matched to standard optical laboratory lens sizing. For thick high-negative diopter prescriptions, we engineer deeper 1.8mm bevel profiles and reinforced 4.0mm to 6.0mm acetate brow sections that completely mask lens edge thickness while preventing lens popping under rapid ambient temperature shifts.
Our turnkey private label services include high-definition pad printing, hot foil stamping, deep CNC metal engraving with enamel infill, and permanent fiber-laser markings. We also fabricate retail-ready presentation accessories: collapsible origami cases, high-density microfiber cleaning cloths with bespoke debossing, GRS-certified recycled PET pouches, and master retail cartons ready for immediate distribution.