

Metal-Acetate Hybrid
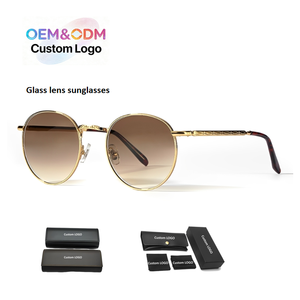
Curated commercial silhouettes combining architectural presence, optical-grade hinge mechanics, and hand-polished cellulose acetate. Available for instant OEM customisation or ODM private-label distribution.
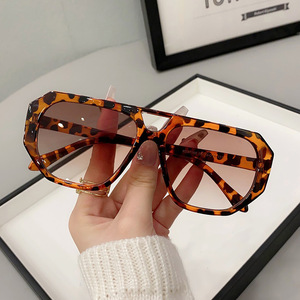
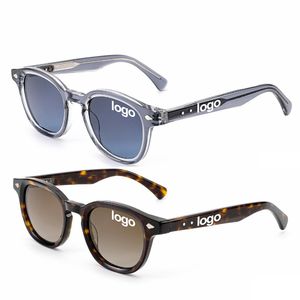
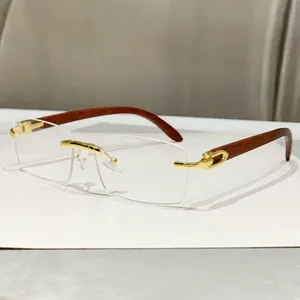
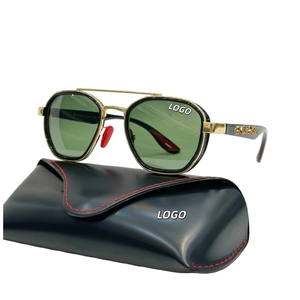
Oversized acetate eyewear demands significantly higher structural integrity than conventional optical frames. Without rigorous curing, internal weight balancing, and calibrated pantoscopic tilt, larger frontages suffer from warping and nasal bridge fatigue.
Our partner manufacturing floors process organic cotton-linter and wood-pulp cellulose flakes aged in climate-stabilised vaults for over 60 days. This degassing protocol prevents plasticizer evaporation post-production, guaranteeing that oversized 8.0mm to 12.0mm rim profiles resist torsional warpage under extreme thermal variances.
Oversized fronts frequently suffer from excessive front-heavy momentum. By deploying multi-axis high-speed CNC routers, we implement interior rim scallop bevels and rear lens-groove stepped recesses. This reduces deadweight by up to 28% while maintaining bold architectural silhouettes from the primary aesthetic angle.
Conventional pinned hinges fail under the cantilevered torque of broad 145mm-150mm temple spans. We engineer lost-wax investment casting titanium alloy hinges and five/seven-barrel Teflon-coated pin assemblies, wire-injected directly into reinforced nickel-silver cores for lifetime articulation without friction loss.
The global eyewear landscape is pivoting from generic private-label reselling toward high-spec bio-circularity, precision regional ergonomics, and compressed rapid-tooling supply cycles.
Global optical retail chains in North America and Western Europe are enforcing strict ESG compliance. Sourcing contracts are transitioning to phthalate-free, biodegradable cellulose formulations with bio-based plasticizer contents exceeding 68% (ISO 14855 biodegradation standards), necessitating verified green supply certifications (ISCC PLUS, OEKO-TEX).
Historic European oversized profiles caused cheek-resting and lens fogging across broader global demographics. Future B2B catalog procurement demands dual-mold bridge availability: built-up 12mm-14mm splayed acetate nose-pads alongside extended mechanical pad-arms to cater simultaneously to high-bridge and low-bridge cranial structures.
The era of rigid 1,200-piece per SKU minimums is concluding. Tier-1 China factories leverage parametric 3D CAD modeling paired with multi-spindle CNC prototyping, allowing independent luxury brands to procure pilot commercial batches of 300 pieces across 3 bespoke acetate sheet acetations within a compressed 35-day production loop.
| Material / Structural Metric | Standard Extruded Plastic (PC/TR90) | Traditional Cellulose Acetate | High-Density Bio-Acetate (Factory Spec) |
|---|---|---|---|
| Raw Formulation | Petroleum Synthetic Pellets | Cellulose Flakes + DEP Plasticizers | FSC Certified Wood Pulp + Bio-Plasticizers |
| Tensile Strength & Rigidity | Moderate (prone to stress crazing) | High (requires core-wire stabilisation) | Ultra-High (retains thin-milled oversized profiles) |
| Thermal Adjustability | Non-Adjustable (fixed memory) | Heat-Formable at 55°C–65°C | Superior Heat Retention at 50°C–60°C |
| Surface Luster & Depth | Surface Spray / Synthetic Coat | 72-Hour Barrel Mechanical Polish | Deep Sectional Refraction + Mirror Buffing |
| Eco-Standard & Biodegradability | Non-Biodegradable (Landfill) | Slow Degradation (Decades) | ISO 14855 Industrial Compostable (>90% in 180 Days) |
A rigorous eight-stage manufacturing continuum guarantees that oversized fronts maintain optical concentricity, hinge friction torque, and skin-neutral surface finishes.
Raw acetate slabs are heat-treated in thermal kilns to equalize molecular stress prior to router indexing, preventing posthumous frame distortion.
Fronts and temples are routed simultaneously. Critical eyewire groove angles are calibrated to standard 110° V-profiles for optical lens retention.
Nickel-free German silver core wires are pneumatic-driven into heated temples, anchored to lost-wax investment titanium hinge joints.
Frames undergo a consecutive 72-hour rolling tumble through birchwood chips, pumice granules, and carnauba wax to achieve razor-free comfort edges.
Essential guidance addressing regulatory certifications, engineering lead times, and structural validation standards for global brands sourcing from top Chinese acetate facilities.
Collaborate with world-class engineering specialists. From rapid 3D prototyping and custom sheet formulations to certified global export fulfillment, we engineer optical excellence for international brands.